Plastic blow molding is a practical manufacturing process for producing bottles, containers, drums, and technical parts at scale. Global buyers must evaluate more than the quoted machine price. Resin compatibility, mold design, wall-thickness control, cycle time, energy use, and after-sales support can determine the real cost of ownership.
PlasticsEurope’s Plastics—The Fast Facts 2024 reports global plastics production of approximately 413.8 million tonnes in 2023. Packaging remained one of the largest application sectors, creating strong demand for lightweight and durable containers. However, this volume does not guarantee a suitable supplier. A machine designed for HDPE bottles may perform poorly with PET or recycled-content materials. Small differences matter. A weak pinch-off can create leaks. Uneven cooling can cause visible paneling.
Industry forecasts also vary widely. Reports from Smithers, Grand View Research, and other market analysts use different product definitions and regional assumptions. Buyers should treat forecast figures as direction, not certainty. Plant trials, sample inspections, and verified production records are more dependable. This guide presents seven plastic blow molding tips for global buyers, covering equipment selection, mold quality, material efficiency, automation, testing, compliance, and supplier reliability. Some recommendations may appear obvious. They are still frequently missed. A lower machine price can become expensive when spare parts arrive slowly, operators lack training, or rejected containers accumulate beside the production line. Careful comparison remains essential.
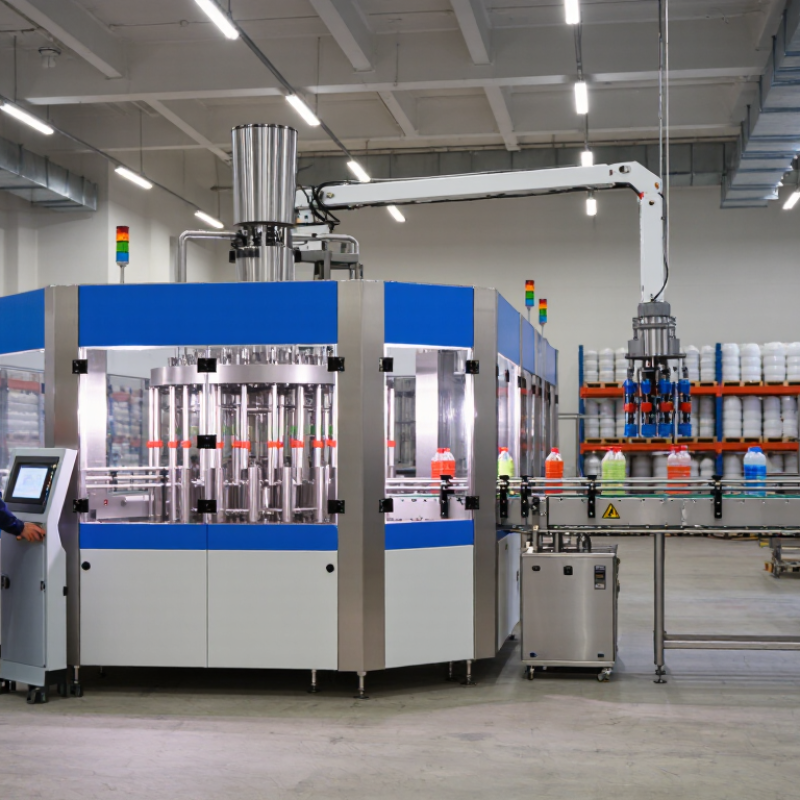
Global buyers should define resin and container capacity before comparing blow molding quotations. HDPE supports a broad range, from small 0.1-liter packs to large 200-liter containers. This flexibility suits personal care, household, industrial, and agricultural applications. PET commonly covers 0.25 to 3-liter containers, especially where transparency, stiffness, and a clean appearance matter.
Start with the resin. HDPE offers impact resistance and reliable chemical performance, but its surface can feel less glass-like. PET provides clarity and stronger visual presentation, yet it may require tighter control of drying, heating, and preform quality. Capacity also changes the process. A 0.1-liter HDPE bottle needs different parison control from a 200-liter container. Wall thickness, handle strength, neck finish, and stacking loads must be checked together.
Ask suppliers for actual samples, dimensional reports, and test data from the proposed machine range. Measure twice. A sample that looks acceptable may still collapse during transport or leak after repeated closure cycles. For PET, inspect haze, base stability, and stress marks. For HDPE, review pinch-off strength, drop performance, and material distribution. Do not assume the largest stated capacity guarantees consistent production. That assumption needs proof. A pilot run can expose cooling delays, uneven walls, or excessive scrap before volume orders begin. Confirm food-contact, recycling, labeling, and transport requirements for each destination market.
For global blow molding buyers, set wall control before requesting quotations. A 1.00 mm target should remain near 0.90–1.10 mm across the bottle body. This ±10% range supports stable strength, appearance, and material use. ISO 20457:2018 stresses controlled moulded-part tolerances, but actual limits depend on geometry, resin, and measurement conditions.
Draft deserves equal attention. Use 2–3° on rigid shoulders, feet, neck transitions, and mould-contacting features. This angle helps release parts without scuffing or forced ejection. Do not apply it blindly to every surface. Thin panels may distort when draft changes local cooling or parison contact. A practical control plan combines parison programming, balanced cooling, and cavity inspection.
Measure real parts, not only CAD files. Check wall thickness at the shoulder, heel, pinch-off, and handle roots with calibrated ultrasonic equipment. Record at least three samples from each production run. The OECD Global Plastics Outlook (2022) reports 460 million tonnes of plastic waste generated globally in 2019, while only 9% was recycled. That figure makes unnecessary resin especially difficult to defend. Still, ±10% can be too ambitious for deep corners or recycled-content grades. That is the uncomfortable part. Buyers should document exceptions, review them with the molder, and revise the design when evidence demands it.
7 Plastic Blow Molding Tips for Global Buyers
Tip 1: Match the resin to the process. EBM suits HDPE containers, especially wide-mouth packs, jerrycans, and built-in handles. The machine forms a hot parison, then traps it inside the mold. ISBM suits PET bottles from 0.25 to 3 liters. It stretches an injected preform for stronger, lighter walls. Do not treat them as interchangeable.
Tip 2: Check the target volume early. A 250 mL PET bottle needs different preform weight and stretch ratios than a 3 L bottle. Tip 3: Confirm the neck finish before tooling. Small mismatches can cause cap leakage. Tip 4: Request wall-thickness maps. EBM may need parison programming around corners and handles. ISBM needs balanced axial and hoop stretching. PlasticsEurope reported that packaging represented 39.6% of European plastics demand in 2022. That scale increases pressure to reduce material waste.
Tip 5: Define barrier needs with evidence. PET may require multilayer structures or coatings for oxygen-sensitive products. HDPE may need additives or barrier layers. Tip 6: Test drop strength, top-load resistance, leakage, and thermal cycling. ASTM and ISO methods help buyers compare suppliers fairly. Tip 7: Audit pilot production, not only samples. A 2024 Smithers PET packaging report identifies lightweighting and recyclability as major market drivers. Yet lightweighting can create unstable bases or thin shoulders. I have seen attractive samples fail after transport vibration. The lesson is uncomfortable: a cheaper mold can become an expensive logistics problem. Ask for process capability data, cavity balance, and a documented corrective-action plan.
HDPE is commonly selected for extrusion blow molding because its density is typically about 0.94–0.97 g/cm³ and it processes well as a durable, opaque container material. PET is commonly selected for injection stretch blow molding, especially for transparent bottles from approximately 0.25 to 3 liters; its typical density is about 1.33–1.39 g/cm³. Actual values vary with grade, additives, and processing conditions.
7 Plastic Blow Molding Tips for Global Buyers
Validate Quality: Apply ASTM D2463, D4169, and ISO 9001 Supplier Records
Tip 1: Request evidence, not promises. ASTM D2463 helps assess drop impact resistance in blow-molded containers. Ask for test conditions, sample size, failure notes, and laboratory dates. A strong report identifies resin type, wall thickness, container volume, and production batch. Photos of damaged samples can reveal brittle corners or uneven bottoms.
Tip 2: Review distribution testing under ASTM D4169. This standard practice examines packaging performance during handling, vibration, compression, and transport. Match the test assurance level to your actual shipping route. Sea freight, air freight, and warehouse stacking create different stresses. Do not accept a generic report. It may not represent your package.
Tip 3: Check the supplier’s ISO 9001 records carefully. Request the certificate scope, current validity, internal audit findings, corrective actions, calibration logs, and batch traceability documents. ISO 9001 supports a controlled quality system, but certification alone does not guarantee perfect parts. Production still needs inspection.
A practical audit should compare records with physical samples. Measure weight, neck dimensions, wall distribution, closure fit, and leakage. Keep retained samples from each approved batch. This creates useful evidence when performance changes later. Some suppliers may provide incomplete records at first. That is not automatically disqualifying, but it deserves written correction, a deadline, and follow-up verification.
| Tip | Quality Dimension | Recommended Verification | Relevant Standard or Record | Buyer Evidence to Request | Acceptance Guidance |
|---|---|---|---|---|---|
| 1 Validate drop-impact resistance |
Container integrity after impact | Test representative blow-molded containers using a defined drop height, conditioning temperature, container fill level, sample quantity, and failure definition. | ASTM D2463 Drop Impact Resistance of Blow-Molded Thermoplastic Containers |
Completed test report, specimen identification, resin lot, conditioning details, drop height, number of failures, photographs, and laboratory date. | Use a buyer-defined pass/fail limit. ASTM D2463 provides the test method; it does not establish one universal acceptance limit for every product. |
| 2 Simulate distribution hazards |
Shipping durability of the filled product and packaging system | Define the distribution cycle, package orientation, vibration exposure, compression or stacking conditions, and post-test inspection criteria. | ASTM D4169 Performance Testing of Shipping Containers and Systems |
Distribution test plan, selected assurance level, test sequence, payload description, conditioning record, and post-test damage report. | Select the test cycle according to the actual transport environment. Acceptance should include no leakage, closure failure, unsafe deformation, or damage that prevents intended use. |
| 3 Review the supplier quality system |
Process control, corrective action, and traceability | Check whether production, inspection, nonconformity handling, calibration, and corrective actions are controlled and documented. | ISO 9001 Quality management system requirements |
Valid certificate scope, audit status, internal audit summaries, corrective-action records, calibration records, training records, and controlled work instructions. | Confirm that the certificate covers the relevant manufacturing activities. Certification alone does not prove that every shipment meets the buyer's specification. |
| 4 Control wall thickness and weight |
Material distribution, container mass, and dimensional consistency | Measure total weight, critical dimensions, and wall thickness at defined locations such as the base, shoulder, body, and neck. | Approved product drawing, control plan, and calibrated measurement equipment | First-article report, in-process inspection sheets, measurement location diagram, equipment calibration status, and statistical trend data. | Set tolerances from the approved drawing and functional requirements. Do not use a single average wall value to hide local thin spots. |
| 5 Verify leak tightness and closure performance |
Leak resistance, sealing surface quality, and closure compatibility | Perform a validated leak test on the container and confirm closure fit, application torque, removal torque, and seal integrity where applicable. | Approved packaging specification, validated leak-test method, and closure-control procedure | Leak-test records, torque results, closure samples, test pressure or vacuum settings, dwell time, and equipment calibration records. | Acceptance limits must match the product risk, filling process, transportation conditions, and regulatory requirements. Record the exact method because leak results are method-dependent. |
| 6 Confirm resin and color consistency |
Material identity, recycled-content control, appearance, and processing stability | Match incoming resin documentation to the approved material specification and inspect color, contamination, black specks, flash, bubbles, weld lines, and surface defects. | Approved material specification, certificate of analysis, incoming-inspection procedure, and lot traceability system | Resin lot number, supplier certificate of analysis, additive or colorant declaration, recycled-content statement when applicable, and retained production samples. | Approve material changes before production. Trace each finished lot to its resin lot and production date so defects can be isolated quickly. |
| 7 Protect lot release and shipment traceability |
Inspection status, quantity control, labeling, and complaint response | Release products only after documented inspection and verify carton labels, pallet identification, quantities, production dates, and lot codes. | ISO 9001 documented-information controls and the buyer's inspection and packaging specification | Final inspection report, certificate of conformity, packing list, lot-code map, retained samples, nonconformity log, and corrective-action response time. | Every shipment should be traceable to a defined production lot and inspection record. Quarantine nonconforming product until authorized disposition is documented. |
7 Plastic Blow Molding Tips for Global Buyers
Calculate Landed Cost: Tooling, Cycle Time, Scrap, Freight, and CO₂ per Unit
For global buyers, unit price is only the visible part of a blow-molded product. A reliable landed-cost model includes tooling, resin, labor, cycle time, scrap, packaging, freight, duties, and inspection. Start with a spreadsheet that places assumptions beside every figure. Divide tooling across realistic lifetime volume, not an optimistic forecast. For example, a $24,000 mold producing 120,000 accepted units adds $0.20 per unit. Demand may fall. Recheck the model monthly.
Tip 1: Measure cycle time using the intended wall thickness, temperature, and cooling setup. A ten-second delay can raise labor and energy costs across millions of cycles. Use accepted units per hour, not machine promises. Include mold changes and cleaning time. These details are often missed.
Tip 2: Model scrap honestly. Record startup waste, trim loss, leaks, color changes, and dimensional rejects. If scrap rises from 3% to 7%, resin and freight costs per good unit increase. Tip 3: Calculate freight and CO₂ per unit from shipment weight, carton utilization, route, and transport mode. Divide transport emissions by saleable units, not produced units. Ask suppliers for measured production and shipment data. Estimates are useful, but they are rarely perfect.